Blog

  • What a COPP Actually Proves — And What It Doesn’t

    A Certificate of Pharmaceutical Product proves three administrative facts and nothing more: that one specific product holds a marketing authorisation in the exporting country, whether that product is actually sold there, and that the site making it has been inspected against WHO GMP. It says nothing about the batch in your container. If you are registering an Indian product for the first time, understanding that boundary will save you a rejection and a wasted authentication cycle at your embassy.

    One product, one certificate

    The WHO guidance is explicit that the certificate “is for a single product only since the manufacturing arrangements and approved information for different dosage forms and different strengths can vary.” A 500 mg tablet and a 250 mg tablet of the same molecule are two certificates. A twelve-product order is twelve certificates.

    This is where most first enquiries go wrong. Buyers ask a manufacturer to “send your COPP”, expecting a single document covering the factory. That document exists, but it is a different one — the WHO-GMP certificate, which covers the site and the categories of product licensed there. The CoPP is the product-level certificate built on top of it. Ask for both, and ask for the CoPP product by product against the exact strengths and pack presentations you intend to register.

    The three lines an overseas regulator reads first

    The WHO model certificate runs to several numbered boxes, but a reviewing assessor goes straight to three of them.

    Box 1.3 asks: “Is this product authorized by the certifying authority to be marketed in the certifying country or within the jurisdiction of the certifying regional authority?” A “No” here is not automatically fatal, but it moves the file into a different queue.

    Box 1.4 asks: “Is this product actually on the market in the certifying country?” — with Yes, No or Unknown as the permitted answers. This is the box that surprises importers. Plenty of Indian-made products are manufactured for export only. Under the CDSCO export No Objection Certificate route, the manufacturer undertakes that “the entire quantity… shall be exported and no part of it will be diverted for domestic sale in India”, and the pack is labelled “For export only – Not for domestic consumption.” That is a lawful, documented arrangement — but it produces a “No” in box 1.4, and some importing authorities treat that answer as a reason to ask for more.

    Box 3.5 asks whether “the facilities and operations of the manufacturer of the FPP conform to good manufacturing practices (GMP) as recommended by WHO.” This is the line the certificate exists for. Read it alongside the site’s WHO-GMP certificate and the date of the last inspection.

    Who issues it, and how long the process takes

    CDSCO administers the WHO certification scheme in India in coordination with the State Licensing Authorities. For a plant in Himachal Pradesh, the application is made to the State Licensing Authority and the inspection is a joint one, carried out by CDSCO zonal or sub-zonal officers together with state representatives.

    How long it stays valid — two answers, not one

    The WHO guidance leaves validity to the issuing authority: “A period of validity can be provided by the authority on the certificate.” There is no universal expiry.

    In Indian practice, WHO-GMP certificates and CoPP have carried a three-year validity since 2018, when the Drugs Controller General extended it from two years. That figure has moved before — in May 2020 CDSCO extended certificates expiring between March and August 2020 by a further six months — so verify the dates printed on the actual document rather than assuming the rule.

    The validity that constrains you, though, is usually the importing regulator’s. NAFDAC, for example, requires that the certificate be issued by the health or regulatory body in the country of manufacture, conform to WHO format, and be authenticated by the Nigerian Embassy or High Commission in the country of origin — with a Commonwealth or ECOWAS mission acceptable where no Nigerian mission exists. The accompanying cGMP certificate must be “valid at the time of submission.” Authentication takes weeks. A certificate with eight months left on it can still be too old by the time your dossier is assessed.

    What a CoPP does not prove

    It does not certify the consignment. WHO deals with individual consignments through a separate instrument — the batch certificate, which “refers to an individual batch” and is described as a vital instrument in the procurement of medicines. The CoPP is for registration; the batch certificate and certificate of analysis are for the shipment. Treating a CoPP as a quality release is a category error, and it is the one that most often shows up in a first-time importer’s file.

    It also does not attest bioequivalence, stability in your climatic zone, or suitability of the pack for your market. Box 4 asks only whether “the information submitted by the applicant satisfy the certifying authority on all aspects of the manufacture of the product” — a statement about that authority’s satisfaction, not a technical opinion you can use in place of data.

    Reading a WHO-format CoPP: the boxes that matter

    BoxWhat it asksWhat to do with the answer
    1.3Is the product authorised to be marketed in the certifying country?If “No”, go straight to box 2.B for the reason before anything else
    1.4Is the product actually on the market there? (Yes / No / Unknown)“No” is normal for export-only products — ask for the export NOC and a specimen of the “For export only” label
    2.A.1Marketing authorisation number and date of issueCheck it matches the exact strength and dosage form you are registering, not a sister product
    2.BIf not authorised, the reason: not required / not requested / under consideration / refused / withdrawal for commercial reasons / withdrawal for sanitary reasons“Refused” or “withdrawal for sanitary reasons” ends the assessment. The others do not
    3.5Do the facilities conform to WHO-recommended GMP?Pair with the site WHO-GMP certificate and the date of the last inspection
    4Does the applicant’s submitted information satisfy the certifying authority?A “No” here is rare and material — ask what was outstanding

    How Salus approaches this

    Salus Pharmaceuticals manufactures at a WHO-GMP and ISO 9001:2015 certified facility in Baddi, Himachal Pradesh, and has done so since 2005. Certification documents are issued product by product through the State Licensing Authority route described above, and export documentation for Nigeria, Bangladesh and Sri Lanka is prepared against each destination regulator’s own authentication and currency requirements rather than as a single standard pack.

    Need COPP documentation for your products?
    [Ask for our current CoPP list, product by product →]

    https://www.saluspharmaceuticals.com/contact.html

  • Diabetes Care in Emerging Markets: Notes from an Antidiabetic Tablets Manufacturer in India

    Antidiabetic Tablets Manufacturer India | Salus Pharmaceuticals

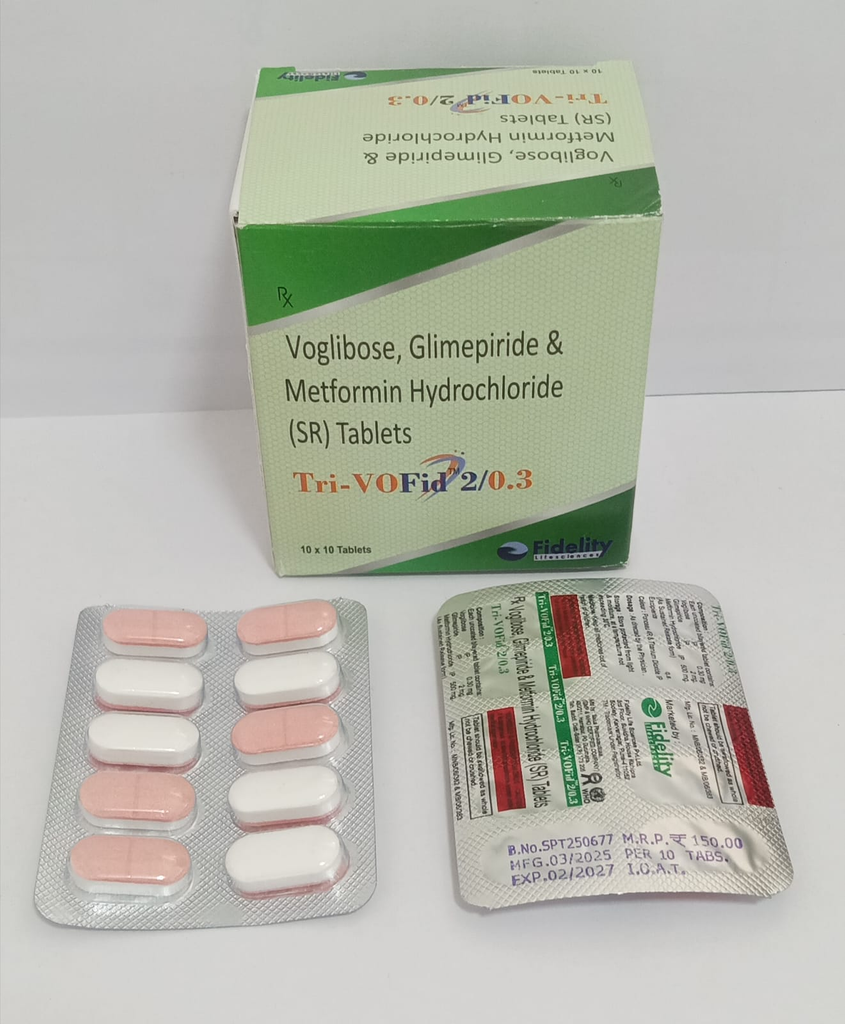
    Three things decide whether a diabetes order works commercially in an emerging market, and none of them is the molecule. Metformin still anchors almost every treatment plan. Price is set by public procurement rather than by the pharmacy shelf. And pack size moves the landed cost more than the active ingredient does. Buyers who understand those three points stop guessing at diabetes tenders and start costing them.

    The demand is concentrated where budgets are thinnest

    The International Diabetes Federation now puts the number of adults aged 20–79 living with diabetes at 589 million, or 11.1% of that age group, rising to a projected 853 million by 2050. That is 45% growth against roughly 25% population growth over the same period — diabetes is outrunning demography.

    The number that matters more to a procurement officer is the undiagnosed one. Around 252 million adults — 42.8% of everyone with diabetes — do not yet know they have it, and 86.9% of those undiagnosed cases sit in low- and middle-income countries. In South-East Asia, 42.7% of the diabetic population is undiagnosed.

    That gap is the forecasting problem. Africa currently records the world’s lowest age-standardised prevalence at 5.0%, but it is not a low-demand market — it is a low-diagnosis market. Every screening programme, every insurance expansion, every new district-level clinic converts undiagnosed prevalence into prescriptions, and the demand curve steps up rather than sloping. If you forecast a diabetes tender on today’s dispensing volumes alone, you will under-order. Forecast on diagnosis capacity instead.

    Metformin still anchors the order book

    The therapeutic conversation has moved on considerably. In September 2025 the WHO added semaglutide, dulaglutide, liraglutide and tirzepatide to its Model List of Essential Medicines — but for a deliberately narrow group: adults with type 2 diabetes who also have established cardiovascular disease or chronic kidney disease and obesity. In the same announcement, the WHO was blunt that “high prices of medicines like semaglutide and tirzepatide are limiting access,” and called for generic competition to bring them down .

    Affordability pressure is structural, not seasonal

    In India, scheduled antidiabetic formulations sit under ceiling prices set by the NPPA under the Drug Prices Control Order. Published research on partial price control of metformin has shown a predictable consequence: when only some strengths and forms are controlled, the market shifts toward combinations and presentations that are not. Any manufacturer quoting an Indian-market diabetes product is quoting inside that structure, and any importer benchmarking against Indian domestic prices should know which side of the schedule they are looking at.

    Export and institutional tenders apply the same pressure by a different route: lowest-evaluated-bid award. On a molecule as commoditised as metformin, no amount of formulation cleverness recovers a bad price. The margin is not in the API. It is in batch size, packing efficiency, yield, and rejection rate — the four things a buyer can actually influence by how they write the enquiry.

    Pack size decides the tender price

    This is the point most enquiries miss. On a low-cost, high-volume tablet, primary packing, carton, insert and shipper can account for a substantial share of ex-works cost. Change the pack configuration and you change the bid.

    The shape of the effect, using illustrative figures — plug in current rates before you rely on them:

    Pack configurationPacking cost per tabletNotes
    10s blisterHighestFamiliar retail pack; most foil and carton per tablet
    15s alu -aluHighCommon private-channel size in South Asia.  Better moisture barrier, fewer cartons per thousand tablets
    100s HDPE containerLowestCheapest per tablet; needs dispensing infrastructure at the clinic.  Strong fit for institutional dispensing

    Two cautions before you optimise straight to the largest pack. First, metformin tablets are physically large, especially at higher strengths, so pack volume drives freight and warehouse cost as well as material cost — a container’s worth of 10s blisters holds far fewer treatment courses than the same container of bulk packs. Second, the pack has to survive the market it ships to: stability at 30°C/75% relative humidity has to be demonstrated for the specific pack you intend to buy, not for the product in general.

    The practical fix is simple. Ask for two or three pack configurations in every quotation, not one.

    Four questions worth putting in the enquiry

    1. Which strengths, and immediate- or sustained-release? These are different manufacturing routes with different costs — settle it before pricing.
    2. Stability data at 30°C/75% RH for the exact pack offered. A quote without pack-specific stability data is not yet a quote.
    3. Blister, alu-alu or HDPE — with a packing cost per tablet for each. This is where the bid is won.
    4. Batch size and minimum order at each configuration. A price that only holds at a batch size you will never order is not a usable price.

    How Salus approaches diabetic care

    Salus Pharmaceuticals has manufactured formulations at its WHO-GMP and ISO 9001:2015 certified facility in Baddi, Himachal Pradesh since 2005, with diabetic care among its 21-plus therapeutic categories. Tablets are supplied in blister and capsules in alu-alu packs, and diabetes enquiries are quoted across more than one pack configuration as a matter of course, because the configuration is usually what decides whether the order is viable.

    Send us the strengths, the annual volume and the destination market, and we will come back with a costing across pack options rather than a single line item.

  • Why Oncology Brands Grow Faster With Salus Pharmaceuticals

    Zero-defect manufacturing isn’t a claim we make — it’s a system we built.

    In oncology, there is no margin for a mix-up. A wrong carton, a delayed invoice reconciliation, an unqualified operator running a compression machine, an audit finding that surfaces six months too late — any one of these can cost a brand its regulatory standing, its market, or worse, patient trust.

    At Salus Pharmaceuticals — a WHO-GMP and ISO 9001:2015 certified formulation manufacturer under the Arvincare Group, based in Baddi, Himachal Pradesh — we took a simple position: the way to eliminate risk for our customers is to remove the human error points from every system that touches their product, their money, and their compliance record.

    Over the last year, we’ve built and deployed a set of purpose-engineered digital systems across our operations. Here’s what they do, and why they matter to any brand — especially in oncology — considering Salus as a manufacturing partner.


    1. CDR / Artwork Version Control — Zero Wrong-Print Risk

    Printed packaging material is one of the most under-appreciated risk points in contract manufacturing. A vendor working off an old email, printing an outdated carton design, can trigger a recall before a single tablet is even packed.

    We built a single source of truth system for every carton, leaflet, cylinder, and printed foil we handle. Only one CDR version is ever “live” per item. Every purchase order for printed material is auto-checked against the master version — if a vendor is quoted or supplied an outdated version, the system flags it automatically before mass printing is ever authorized. No print run proceeds without a system-verified “OK TO PRINT.”

    What this means for you: your artwork is protected from the moment it’s approved to the moment it reaches a carton — with a full change log proving exactly when and why each version changed, ready for any auditor who asks.

    2. CRM & Collections FMS — Transparent, Verifiable Business Dealings

    Every commercial relationship runs on trust in the numbers. Our CRM Collection system tracks every invoice, every receipt, and every ageing bucket — with receipts verified independently by Accounts, never by the person managing the relationship. A 100-point scorecard and automated integrity checks mean nothing slips through informally.

    What this means for you: full visibility into your account status at any time, with a system that makes disputes and reconciliation errors structurally rare rather than something you have to chase down.

    3. APQR Format Pack & FMS — Audit-Ready Quality Data, Always

    Annual Product Quality Reviews are where regulatory relationships are won or lost. Our APQR system runs across 21 standardized formats with built-in Cp/Cpk statistical analysis, a data-provenance log for every figure, and completeness gates that block a review from closing until every data point is verified and sourced.

    What this means for you: when your regulatory team — or a WHO inspector, or a third-party auditor — asks “show me the trend data behind this batch,” the answer is one query away, not a week of digging through files.

    4. Self Inspection FMS — Continuous Compliance, Not Once-a-Year Panic

    Self-inspection under Schedule M and WHO-GMP isn’t a checkbox exercise for us. Our system enforces the independence of every auditor, guarantees full coverage across all areas due for review, and — critically — makes retroactive date changes on any inspection impossible, because entries are locked in through a form-driven, timestamp-verified process the moment they’re submitted.

    What this means for you: the audit trail you’re relying on for your own regulatory submissions is real, timestamped, and cannot be quietly edited after the fact.

    5. Tablet Production Operator Scoring — Consistent Hands on Every Batch

    Batch-to-batch consistency starts with the people running the machines. We track operator qualification, machine-specific competency, and run-level performance across all 13 machines on our compression, coating, and granulation lines — with a scoring model that actively rewards operators for self-reporting errors and penalizes errors only caught later by audit or QA. That single design choice changes behavior: operators tell us the truth early, instead of hiding a deviation and hoping it isn’t found.

    What this means for you: the operator standing at the machine producing your batch is qualified for that exact machine, and the incentive structure around them is built to surface problems before they become yours.


    The Common Thread: Systems That Can’t Be Gamed

    Every system above shares the same design DNA:

    • No hand-typed dates. Every timestamp comes from a system source — a form submission, a master record — never a manual entry that could be backdated.
    • Segregation of duties, enforced by the system itself. The person being evaluated can never be the person who signs off on the evaluation.
    • Traceability by default. ALCOA+ principles aren’t a training slide here — they’re built into how data is captured, so every number has a verifiable origin.

    This isn’t compliance theater. It’s infrastructure that happens to make audits painless as a byproduct of making the underlying operations genuinely more reliable.

    Why This Matters More in Oncology

    Oncology formulations carry tighter tolerances, higher scrutiny, and less room for the kind of “we’ll fix it next batch” thinking that other therapeutic categories can sometimes absorb. A partner whose quality systems are built to withstand a WHO inspector’s toughest question — and whose commercial systems are built to withstand your own finance team’s toughest reconciliation — is a partner you can scale with, not just contract with.

    What This Means for Your Growth

    When your contract manufacturer has removed the error points from packaging, quality documentation, self-inspection, operator performance, and commercial reconciliation, the compounding effect shows up in your business, not just ours:

    • Faster regulatory approvals — because your dossiers are backed by audit-ready, provenance-tracked data from day one.
    • Fewer recalls and market-risk events — because the packaging error that caused a 50,000-unit misprint elsewhere in the industry is structurally prevented here.
    • Predictable, disputable-free commercial dealings — so your finance team spends time growing the relationship, not auditing it.
    • A partner that scales with you — because these are systems, not individual heroics, which means the reliability holds as volumes grow.

    We keep building. Every one of these systems started because something went wrong once, and we decided the right fix wasn’t “be more careful” — it was “build a system where the error can’t happen quietly again.”

    That’s the partnership we’re offering.


    Salus Pharmaceuticals — WHO-GMP & ISO 9001:2015 certified formulation manufacturer, Arvincare Group, Baddi, Himachal Pradesh.

  • In Loving Memory of Sandeep Chaubey Ji

    In Loving Memory of Sandeep Chaubey Ji

    Our PPIC Head, Our Colleague, Our Friend

    22 January 2021 – 7 August 2023

    There are days a company remembers not because of a milestone or a target achieved, but because of a loss that changes everything. 7th August 2023 is one such day for us — the day we lost Sandeep Chaubey Ji.

    A Man Who Held the Line

    Chaubey Ji joined us on 22nd January 2021 and took on the responsibility of heading our PPIC (Production Planning and Inventory Control) department — a role that demands precision, patience, and an unshakeable sense of responsibility. Every day, countless decisions pass through PPIC that keep a factory running smoothly: what gets produced, when, in what quantity, and how the material flows to make it all possible. Chaubey Ji carried that responsibility with a quiet dedication that the whole factory came to rely on.

    He wasn’t just punching in and out. He was the kind of employee who showed up — every single day, in every sense of the word.

    The Day We Lost Him

    On 7th August 2023, like any other working day, Chaubey Ji set out for the factory. The staff car that would normally have picked him up didn’t arrive that day — the driver was off. Instead of waiting or turning back, he did what he always did: he found a way to get to work. He set out on his bike.

    He never made it.

    He met with an accident on the road that day and lost his life — on his way to the very factory he had served so faithfully for over two and a half years.

    It is impossible to write that sentence without pausing. A day that should have been ordinary became the darkest day in our company’s history.

    Why We Still Remember Him

    Loyalty is a word that gets used often and means little most of the time. Chaubey Ji gave it real meaning. He was the kind of colleague who didn’t need to be asked twice, who showed up even when the circumstances made it harder, who took ownership of his department and his people.

    Since that day, not one of us who worked with him has stopped thinking about him from time to time — a decision that reminds someone of how he used to plan things, a quiet moment in the PPIC office, an anniversary that passes on the calendar. He is remembered not out of obligation, but because he genuinely earned that place in our memory.

    A Tribute, Not a Farewell

    We don’t write this to say goodbye — that already happened, far too soon and far too suddenly. We write this because some people deserve to be spoken of, remembered out loud, and not just carried silently.

    To Sandeep Chaubey Ji: thank you for your years of dedication, for the trust you built, and for the example you set of what it means to be truly committed to one’s work and one’s team. You are missed more than words can capture, and you remain, and always will remain, a part of this company’s story.

    Rest in peace, Chaubey Ji. You will not be forgotten.

  • Three Generations, One Vision: The Story Behind Salus Pharmaceuticals

    From a wholesale medicine stall in Kurukshetra to exports reaching 13 countries — how one family’s honesty and hard work became a pharmaceutical legacy.


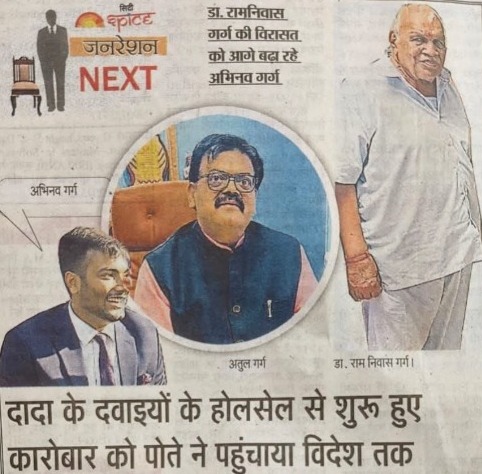
    Every great pharmaceutical company has a first prescription, a first customer, a first act of trust. Ours goes back to 1970, to a small wholesale medicine business in Kurukshetra, Haryana, started by Dr. Ram Niwas Garg.

    There was nothing extraordinary about the beginning — just a young man building relationships with customers one honest transaction at a time. But that honesty became the foundation on which an entire family business would one day stand.

    A Second Generation Takes the Leap

    Inspired by his father’s business, Mr. Atul Garg moved to Panchkula in 2006, carrying forward the same spirit of trust that Dr. Ram Niwas Garg had built. What began as a trading partnership in Parwanoo eventually became something Atul Garg would build entirely on his own — in 2008, he struck out independently.

    The turning point came in 2010, when trading gave way to manufacturing: the family’s first pharmaceutical production facility was set up. Growth followed steadily, and by 2018, a second facility had joined the first — a sign that the business was no longer just surviving, but scaling.

    The Grandson Who Took It Global

    Around the same time, Abhinav Garg — Atul Garg’s son and Dr. Ram Niwas Garg’s grandson — was coming of age. In 2017, he completed his MBA in Family Business Management in Mumbai, arriving with a clear intent: to take what his grandfather and father had built and give it a global footprint.

    Today, that intent has become reality. The group’s manufacturing facilities span Paonta Sahib and Baddi, with a head office in Sector-12A, Panchkula. The business now works with 2,500+ distributors and exports medicines to 13 countries — a scale that would have been unimaginable from that first wholesale counter in Kurukshetra.

    As Abhinav Garg put it:

    “This is a small step towards realizing my grandfather’s dreams. His vision remains my inspiration.”

    What Stayed the Same

    What’s notable about this journey isn’t just the growth — it’s what didn’t change along the way. The same principle that built customer trust in 1970 is the one guiding the business today: quality and integrity, applied consistently, at every stage of growth.

    In Abhinav Garg’s own words, the goal has never been to replace what his grandfather built, but to honor it:

    “Preserving my grandfather’s legacy, I’ve advanced the business with modern technology and new thinking — from the modest scale where it began to a name the industry now trusts.”

    Where Salus Pharmaceuticals Fits In

    This family legacy is the foundation on which Salus Pharmaceuticals’ Baddi facility stands today, under Abhinav Garg’s leadership. Our WHO-GMP and ISO 9001:2015 certified manufacturing, our commitment to affordable and effective medicines, and our expanding presence across global markets are a continuation of the same values that started this story more than five decades ago: earn trust, do the work honestly, and let the results speak.

    Three generations. One vision. And a business that’s still just getting started.


    Story reference: Dainik Jagran, Panchkula edition — “Generation Next” feature on Dr. Ram Niwas Garg’s legacy carried forward by Abhinav Garg.

  • The Women Behind the Manufacturing Floor: Skills We Need to Recognise

    The Women Behind the Manufacturing Floor: Skills We Need to Recognise

    Working in pharmaceutical manufacturing has taught me something that is easy to miss when you only look at designations and organisational charts.

    Some of the most valuable skills in a manufacturing organisation are built on the shop floor.

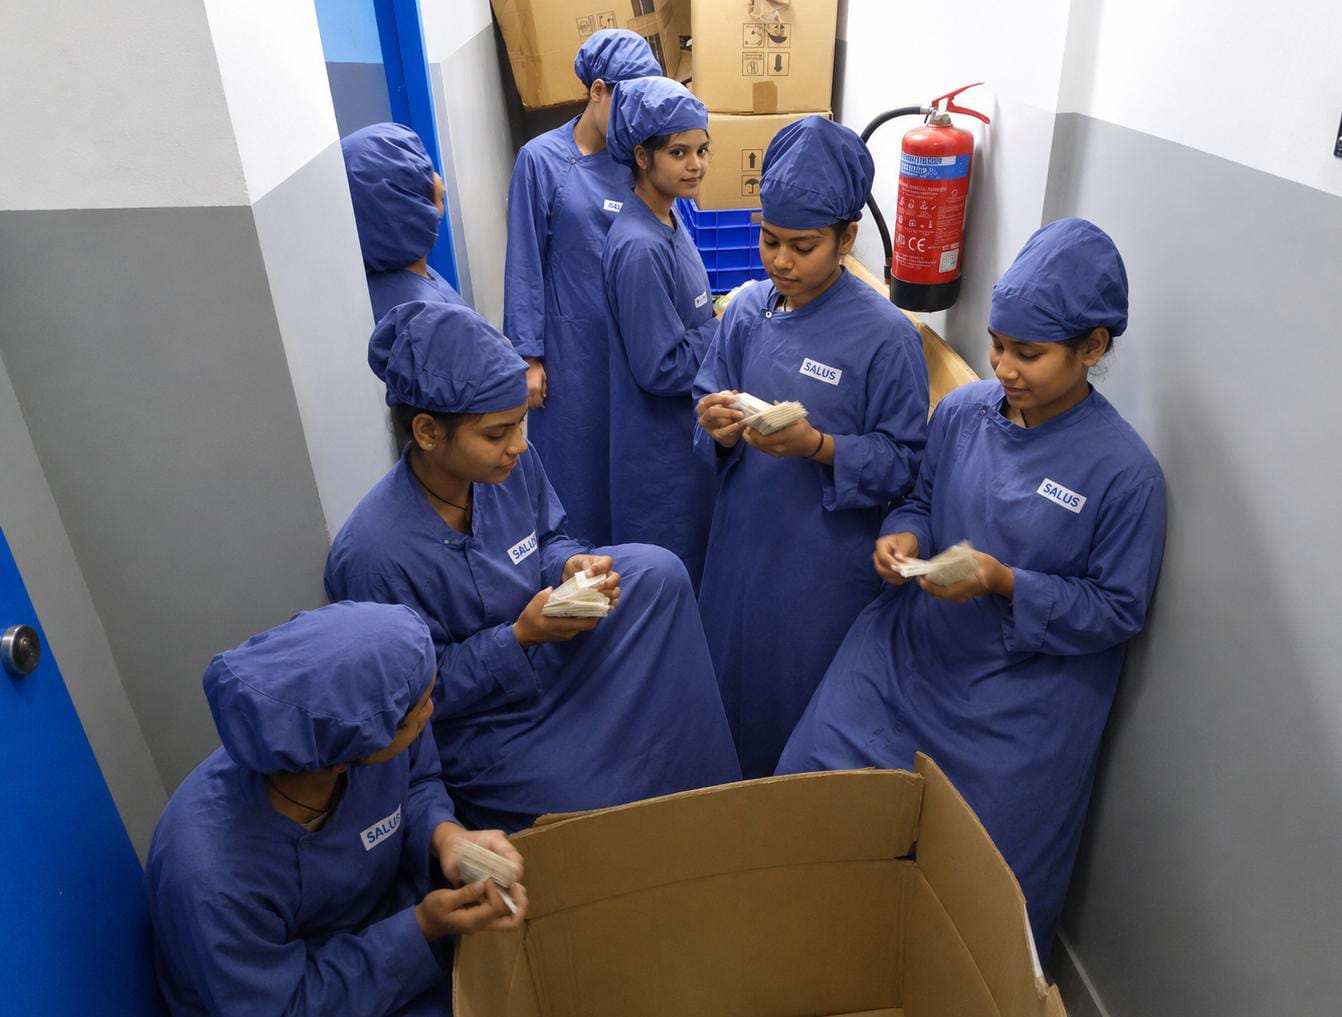
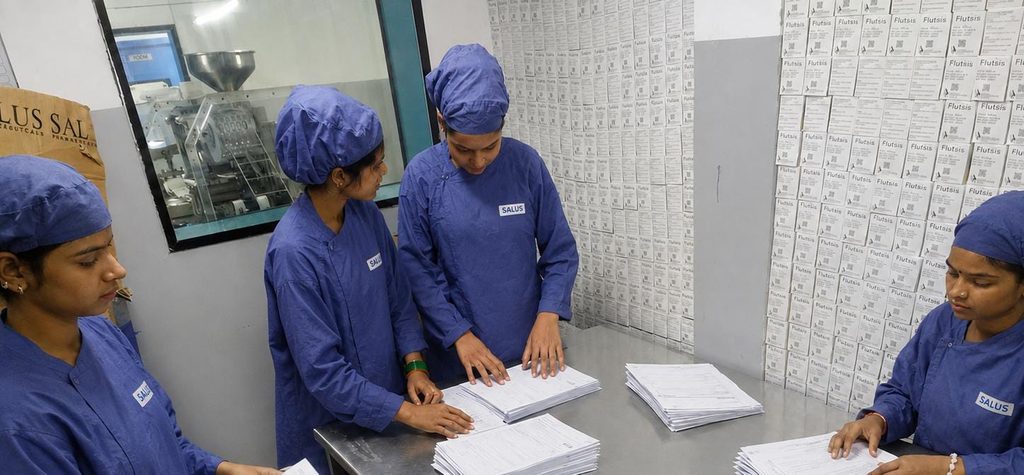
    At Salus Pharmaceuticals, I have had the opportunity to see women contribute across different stages of manufacturing and quality operations—handling processes with discipline, maintaining consistency, performing in-process checks, supporting documentation, managing packing activities and ensuring that every step is carried out with attention to detail.

    From the outside, some of these responsibilities may appear routine.

    They are anything but routine.

    Female worker handling boxes on the pharmaceutical manufacturing floor

    Pharmaceutical manufacturing demands precision. A small variation can affect quality. A missed step can affect an entire batch. Consistency is not simply expected—it is essential.

    And this is where experience on the manufacturing floor becomes incredibly valuable.

    A person who has spent years working around a process develops an understanding that cannot always be taught through a classroom or a manual. They begin to recognise when something is not moving as it normally should. They understand the importance of sequence, cleanliness, documentation, line clearance and process discipline.

    That is expertise.

    Yet, too often, we measure careers only through promotions, titles and formal qualifications, while overlooking the practical knowledge people accumulate through years of doing the work.

    Women working in manufacturing deserve to be recognised not simply for being part of the workforce, but for the technical understanding, discipline and process knowledge they bring to the organisation.

    At Salus Pharmaceuticals, I believe manufacturing is not just about machines, systems and technology.

    It is about people who understand those systems, respect the process and take responsibility for the quality of what ultimately reaches a patient.

    And when we talk about the future of pharmaceutical manufacturing, we should make sure that women on the manufacturing floor are part of that conversation—not invisible within it.

    Because behind every compliant batch and every quality product, there are people whose experience, attention and discipline make it possible.

    Female workers handling documents on the pharmaceutical manufacturing floor

    It is time we recognise that contribution.

  • How Salus Pharmaceuticals Improved Pharmaceutical Manufacturing Operations

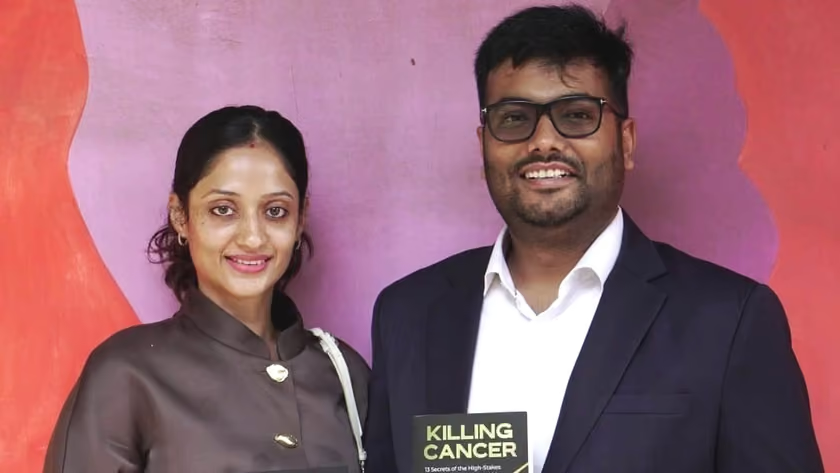
    Mehak Aggarwal and her husband are the third generation running their family’s pharmaceutical manufacturing business. Salus Pharmaceuticals operates a WHO GMP certified plant in Baddi, Himachal Pradesh, manufacturing tablets, capsules, and injections, including oncology products. A second unit, Sunvet Healthcare in Kala Amb, makes eye drops. The Baddi plant alone runs on around 300 people, 107 of them staff.

    That is not a small operation. Pharma manufacturing is one of the most documented, most audited, most process heavy industries in India. Every batch has a record. Every deviation has a form.

    And yet both owners were inside the plant seven days a week.

    That was Mehak’s own description of her weeks. Not strategy. Not expansion. Manpower and production fires, every single day, in a business that was already third generation and already certified to global standards.

    These challenges can have a direct impact on pharmaceutical manufacturing operations, especially when manpower and production activities are managed manually.

    Why Data Matters in Pharmaceutical Manufacturing

    Here is the uncomfortable question. If a pharma plant already generates this much data, why were two capable owners still finding problems by standing on the floor?

    Because data sitting in registers and batch records is not the same as data an owner can read. Nobody had translated the plant into a form that answered the only question that matters at the top: where is today’s bottleneck?

    Using production data effectively can help pharmaceutical manufacturers identify bottlenecks, monitor operations, and make faster business decisions.

    The gap was never capability. Mehak and her husband run a plant that clears WHO GMP audits. The gap was that no tool existed to show them the business without them physically walking it. Someone had to sit with them, name the problem in their own language, and build the tools alongside them. That work took months, one dashboard at a time, and every dashboard removed one more reason to be on the floor.

    Dashboards for Pharmaceutical Manufacturing Operations

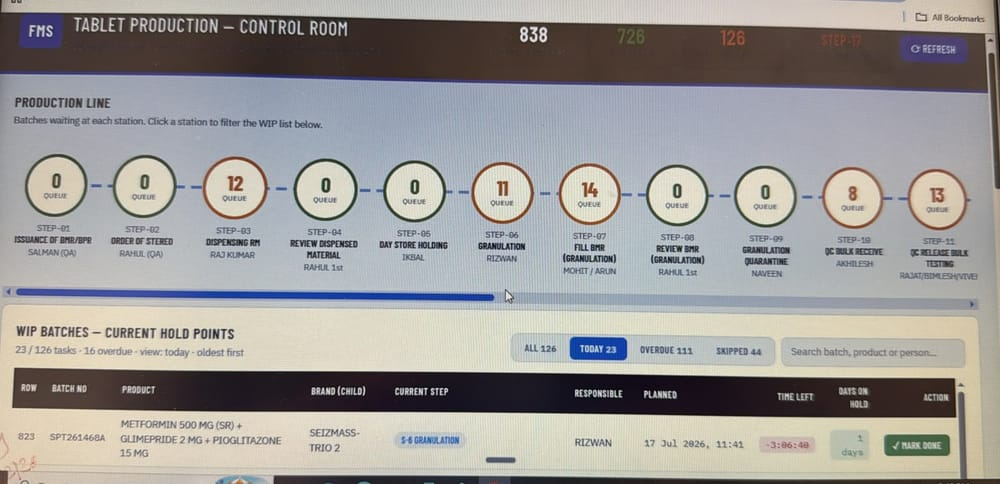
    Dashboards. Not one master dashboard, but a set of them, built together over months of working side by side, each one answering a specific operational question.

    We have built together lots of dashboards which now help me identify the bottleneck in just seconds

    Seconds. The thing that used to take a full day of walking the floor, asking supervisors, and cross checking registers now takes seconds from anywhere. This data-driven approach has made pharmaceutical manufacturing operations more efficient and easier to monitor.

    The Pharmaceutical Manufacturing Dashboard :

    Here is what that changed in practice:

    BeforeNow
    Seven days a week inside the plantOne day a week. Monday.
    Bottlenecks found by walking the floorBottlenecks identified in seconds on a dashboard
    Chasing employees for updatesEmployees run on the system, not on reminders
    Late nights and business talk at the dinner tableEvenings, weekends, and trips are theirs again


    Results: Improving Pharmaceutical Manufacturing Operations

    The numbers first. Time inside the plant dropped from seven days a week to one. Attrition dropped from 6% to 2.1%, because a team that is not being chased every day is a team that stays.

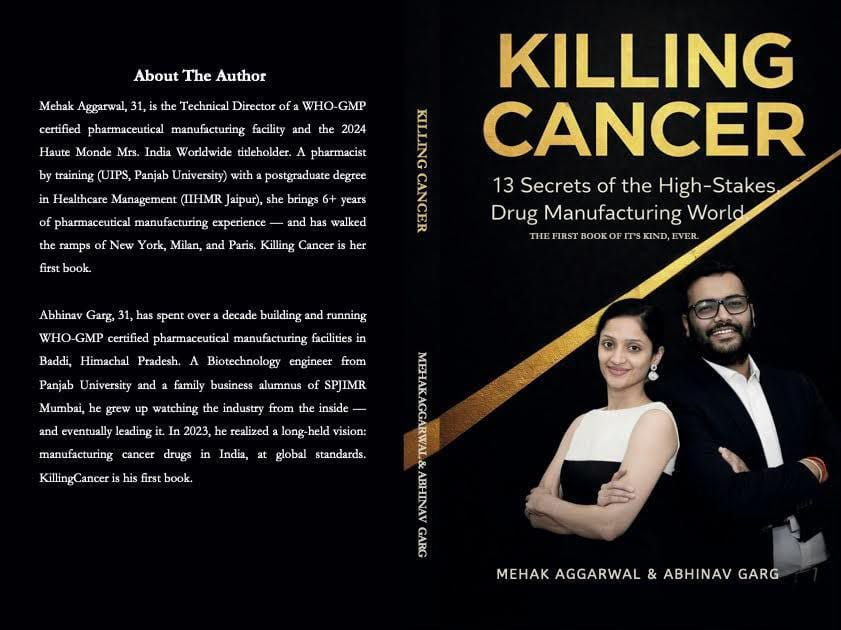
    Then the compounding effect. With the plant no longer consuming every waking hour, the couple did something most manufacturers never find the bandwidth for. They wrote and launched a book, Killing Cancer: 13 Secrets of High-Stakes Pharma Manufacturing, with a media launch that got covered in more than 14 newspapers.

    The Book
    That is what the freed hours became. Not rest alone. Higher order work .

  • What the Factory Floor Teaches That No Classroom Can

    A pharmaceutical factory can teach lessons that are difficult to learn anywhere else.

    A person may enter a company on the first day with a degree, knowledge, confidence or even a strong family background in business. Four years later, the same factory can look completely different to that person.

    Not because the building has changed.

    Because the person has.

    Working inside a manufacturing environment exposes people to realities that cannot be fully understood through classrooms, textbooks or business plans. Decisions have consequences. Processes have limits. Small details matter. And problems rarely arrive in the neat format of a case study.

    That is one of the ideas explored in Killing Cancer.

    The book looks at pharmaceutical manufacturing from the perspective of people who have actually experienced the industry from within—not simply from the outside looking in.

    And perhaps that is why the factory floor can be such a powerful teacher.

    It does not ask where someone studied, what degree they hold or what family they come from.

    It asks a much simpler question:

    Can you understand the reality in front of you—and can you make the right decision when it matters?

    He Didn’t Start on the Factory Floor by Choice

    At 21, Abhinav Garg entered the company with a very different expectation of what his professional journey would look like.

    His first assignment was not a boardroom role, a client-facing position or a carefully designed management position. He was placed as a packing supervisor.

    And he did not enjoy it.

    The noise of the machines was unfamiliar. The job did not feel like the destination he had imagined for himself. Within days, he was already thinking about leaving.

    But then something changed.

    He remembered what his family had told him about working his way up rather than simply expecting a position because of his background. He also began observing the senior people around him—how they handled the factory, the people, the problems and the pressure.

    The change did not happen overnight.

    Over the following weeks, his perspective began to shift gradually. The pauses became shorter. The discomfort became more manageable. And slowly, he began earning something more important than a designation: the right to belong on the factory floor.

    That distinction matters.

    A position can be given.

    The credibility to handle that position has to be earned.

    And perhaps that is one of the most important lessons a factory can teach—especially in pharmaceutical manufacturing, where practical understanding cannot simply be inherited, assigned or learned from a job title.

    A Different Kind of First Day

    Four years later, the same factory saw another first day—but this time, the challenge looked very different.

    By 2020, Mehak Aggarwal had already built a strong professional foundation. She held a Bachelor of Pharmacy from UIIP, Panjab University, a postgraduate degree in Healthcare and Hospital Management from IIHMR Jaipur, and years of administrative experience at PGIMER Chandigarh and Indus Hospitals.

    She was not unqualified.

    She was not inexperienced.

    She had studied pharmacy, managed people, worked in high-pressure healthcare environments and understood the responsibilities that came with administration.

    But stepping into pharmaceutical manufacturing as a Technical Director was different.

    Her previous qualifications could not automatically establish her credibility on the production floor. She was new to manufacturing, and she was entering a production environment that had traditionally been dominated by men.

    There was another layer to the perception around her: she was the Managing Director’s wife.

    Nobody needed to say directly that this mattered. Sometimes, you simply feel it through the way people look at you, observe your decisions and wait to see what you can actually do.

    And the factory floor was about to give her that answer.

    During her very first week, a discussion with the production planning team turned into an unexpected challenge. A senior operator, with roughly two decades of experience on the floor, openly disagreed with her approach.

    His message was clear: a new way of doing things could not simply replace what experienced operators had learned over years of working with the process.

    It would have been easy to turn the conversation into a contest of authority.

    Instead, Mehak chose to listen.

    She began asking why the operators worked the way they did. What had their experience taught them? What did they know about the machines that could not be understood from a report or a meeting room? What practical problems had shaped the existing process?

    Rather than trying to prove her point immediately, she started understanding the factory itself.

    And this is where the factory floor teaches a lesson that classrooms rarely can.

    An idea may sound right in a meeting. Production will test whether it actually works.

    Over time, the relationship with the same senior operator changed.

    The person who had initially challenged her eventually became one of her most reliable collaborators.

    Not because she won the argument.

    Not because she used her position.

    But because the evidence accumulated.

    That experience captures something fundamental about pharmaceutical manufacturing: credibility is not created by a designation alone.

    A degree can demonstrate knowledge.

    A position can establish responsibility.

    Experience can provide perspective.

    But on the factory floor, evidence is what earns trust.

    And perhaps that is why the same factory can humble someone on their first day and, years later, become the place where they develop the confidence to make better decisions.

    What Day One Teaches You

    These two stories are not important because they are stories of struggle or because they are meant to create sympathy.

    They matter because they reveal something much more fundamental about pharmaceutical manufacturing.

    On the first day, people may arrive carrying qualifications, certificates, professional experience and a family name that already carries weight outside the factory.

    But the factory floor does not evaluate people by what they bring on paper.

    It evaluates what they actually know, how well they understand the process, how they respond to problems and whether they can contribute when the work becomes real.

    A degree can tell people what you have studied.

    A designation can tell them what responsibility you have been given.

    A family name can tell them where you come from.

    None of these can substitute for understanding the work.

    That understanding has to be built through observation, experience, questions, mistakes, evidence and repeated decisions on the floor.

    That is what connects the two journeys.

    One person entered the factory without wanting the role he was given. Another entered it with qualifications and professional experience but was still new to manufacturing.

    Both eventually discovered the same thing:

    The factory floor does not care who you are outside it. It cares about what you know, what you learn and what you can prove inside it.

    And perhaps that is the first and most fundamental lesson of pharmaceutical manufacturing:

    The factory floor is where credentials meet reality.

    Secret : The Factory Floor Is the Real Classroom

    In pharmaceutical manufacturing, success does not automatically come with a degree.

    It does not come with a family name either.

    And it certainly does not come simply because someone has been given an important designation.

    The factory floor has a different way of measuring capability.

    It quickly reveals what you know—and, perhaps more importantly, what you do not know yet.

    That can be uncomfortable.

    Someone may enter a manufacturing environment with years of education, professional experience or a strong background in business. But the moment that person begins working with actual processes, equipment and experienced operators, a different kind of learning begins.

    The smartest response is not to pretend to know everything.

    It is to become willing to learn from the people who have been there the longest.

    Operators often carry a kind of practical knowledge that does not appear in a textbook. They have seen equipment behave differently under real conditions, encountered problems before they became formal deviations, and learned which details can matter during production.

    This does not mean formal education is unimportant.

    It means classroom knowledge and factory-floor knowledge solve different parts of the same problem.

    Every role on the floor can become a learning opportunity if you approach it like a student. And the factory itself can become a classroom—one where lessons are taught through real situations rather than theory alone.

    But knowledge is only one part of the equation.

    Respect is earned over time.

    It grows through consistent presence, understanding the work and being there when things become difficult—not only when everything is running smoothly.

    That is why people who spend years on the factory floor can sometimes possess a depth of practical knowledge that cannot be measured by their academic qualifications alone.

    Their knowledge has been built through repetition, observation, problems and experience.

    And there is another important lesson here: if you want to understand manufacturing, be present on the floor.

    Not just when there is a crisis.

    Not just when something has gone wrong.

    Be there when production is running normally. Observe. Ask questions. Understand the process. Learn how people work with the equipment.

    Because when a real problem eventually appears, you will already understand the environment you are trying to solve it in.

    The factory floor does not ask:

    “What degree do you have?”

    It asks:

    “Do you understand the process—and are you willing to keep learning?”

    That may be the first secret of succeeding in pharmaceutical manufacturing:

    Credibility begins with the humility to learn, and grows through consistent presence.

    Takeaways: What the Factory Floor Really Teaches

    • A degree can open the door, but it cannot replace practical knowledge.
    • The factory floor quickly reveals what you know—and what you still need to learn.
    • Experienced operators carry practical knowledge that cannot always be found in textbooks or formal documents.
    • Credibility is earned through presence, observation, consistency and evidence—not simply through a designation or family background.
    • New ideas should be tested against real manufacturing conditions, not defended through authority alone.
    • Listening to the people closest to the process can lead to better decisions.
    • When problems arise, the people who understand the floor are often better positioned to understand what is actually happening.
    • In pharmaceutical manufacturing, knowledge becomes stronger when formal education meets hands-on experience.

    The Problem With Calling a Change “Small”

    Imagine a manufacturing team decides to alter the mixing time of a process.

    The equipment remains the same.
    The raw material remains the same.
    The product name remains the same.

    So, is it really a major change?

    Not necessarily.

    But the important question in pharmaceutical manufacturing is not simply “What changed?”

    It is:

    “Could that change affect the process or the quality of the finished product?”

    WHO guidance makes this distinction important. Changes to procedures, processes and methods are expected to be managed through an appropriate change-control system, with the need and extent of validation or revalidation determined through risk management.

    That means the word small can be misleading.

    A small change in an input, process parameter, piece of equipment or packaging component may deserve a much larger investigation than its physical size suggests.

    What Happens After the Change?

    This is where the factory floor becomes interesting.

    A pharmaceutical process is not judged only by whether the machine continues running.

    Manufacturers need evidence that the revised process can still consistently produce a product meeting its predefined quality requirements. WHO guidance on change management calls for sufficient data to demonstrate that a revised process will result in a product of the desired quality and consistent with approved specifications.

    So a change can create a chain like this:

    Change → Risk Assessment → Change Control → Validation/Revalidation Decision → Evidence → Continued Monitoring

    The important part is the middle of that chain.

    The decision is not simply about whether production can continue. It is about whether there is enough scientific and documented evidence to show that the process remains under control.

    Why “It Worked Before” Is Not Always a Good Answer

    One of the most dangerous assumptions in manufacturing is that because a process worked yesterday, a modified version will automatically work tomorrow.

    Pharmaceutical manufacturing deals with variability.

    Raw materials can differ. Equipment can change. Processes can evolve. Suppliers can change. Manufacturing conditions can be modified.

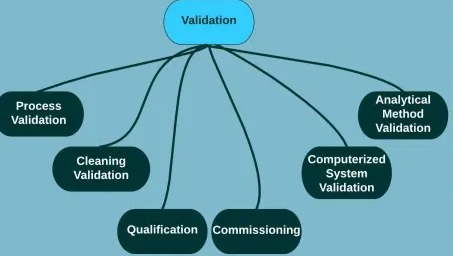
    That is why process validation is not simply a one-time certificate that a process is “good.”

    WHO describes process validation as documented scientific evidence that a process is capable of consistently delivering products of the required quality. Its guidance also emphasizes monitoring and evaluating process performance throughout the product lifecycle.

    In other words:

    The goal is not to prove that one batch worked.
    The goal is to understand whether the process can keep working consistently.